Skip to content
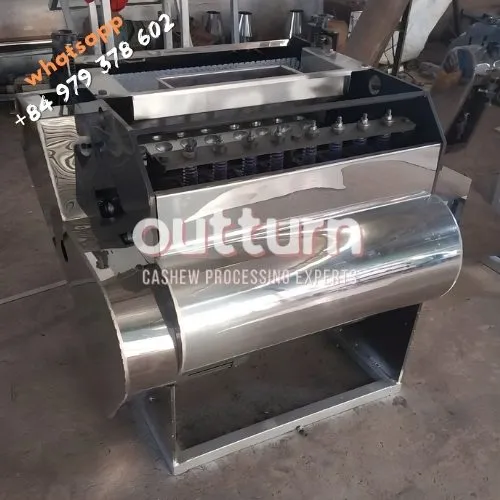
OUTTURN 10-head cashew nut cutting machine with ten rotary cutting cups on a steel frame
200–240 kg/hrUp to 76% Outturn

10-Head OUTTURN Cashew Nut Cutting Machine

SKU: OUTTURN-CCM-10H

Factory-Direct Pricing — Request a Quote

Cutting heads
10 rotary cups
Motor power
1.1 kW (1.5 HP)
Rated capacity
200–240 kg/hr steamed RCN
Typical outturn
Approx. 76%
Voltage
380V, 3-phase, 50 Hz (220V single-phase on request)
Blade material
Special alloy steel, field-replaceable
Machine weight
Approx. 165 kg
Footprint
Approx. 1.8 m x 0.9 m x 1.2 m (L x W x H)
Broken kernels (cutting stage)
Under 3%; under 1% with well-graded, evenly steamed RCN
Uncut nuts (cutting stage)
Under 5%; lower still by reducing motor speed
Blade care
Clean daily, sharpen weekly, replace every 2–3 months depending on workload
Spare parts
Made in-house at our factory: genuine parts at factory-direct prices

How the 10-Head OUTTURN Cutting Machine Works

A step-by-step look at how steamed raw cashew nuts move through the 10-head OUTTURN machine, from loading to shelled kernel output.

  1. 1

    Steam and condition the RCN

    Raw cashew nuts are steamed or boiled ahead of time so the shell softens and separates more cleanly from the kernel during cutting. Nuts should be sized and dried to a consistent moisture level before they reach the machine.

  2. 2

    Load nuts into the feed cups

    An operator manually places one steamed nut into each of the machine's cutting cups. On the 10-head model, ten cups are filled per cycle, which is what allows this size machine to sustain a higher hourly throughput than smaller head counts.

  3. 3

    Cups rotate into the blade plane

    The 1.1 kW (1.5 HP) motor drives a central shaft that rotates all ten cups in sequence through a fixed cutting blade. Each cup carries its nut through the blade plane at the same cutting height, so shell thickness and kernel size are treated consistently across every cup.

  4. 4

    The blade splits the shell along the seam

    As each cup passes the blade, the pressure and angle are set to score and open the shell rather than force it, which reduces breakage of the kernel inside. The blade edge is special alloy steel and is replaceable as it wears.

  5. 5

    Cut shells and kernels are unloaded

    Once a cup completes its pass through the blade, the operator lifts the opened shell away and extracts the kernel by hand. Loading and unloading continue in a rolling cycle so the motor and blade run continuously rather than stopping between nuts.

  6. 6

    Kernels move on to peeling and grading

    Cut kernels are collected for the next stage of processing — typically drying, peeling of the testa, and grading — which are handled by separate equipment or manual stations downstream of the cutting machine.

The 10-head OUTTURN cutting machine is built for cashew processors who have outgrown a 6- or 8-head line but are not yet ready for a fully automatic system. With ten cutting cups running off the same field-proven mechanism used across OUTTURN’s entire manual line, it is rated for 200–240 kg/hr of steamed raw cashew nuts and a typical outturn around 76%.

A shared design, scaled by cutting stations

Every OUTTURN cutting machine, from the 2-head entry model up to the 12-head, is built around the same core idea: a single motor drives a shaft that rotates cutting cups into a fixed blade plane. Rather than fitting a proportionally bigger motor to each larger model, OUTTURN scales throughput mainly by adding more cups and blade positions around that shaft. The 10-head machine simply has more cutting stations turning through the blade per cycle than a 6- or 8-head unit, which is what pushes its rated capacity toward the 200–240 kg/hr range.

Motor size does step up at the top of the range, but far more slowly than capacity. The 2- through 8-head machines all run a 1 HP (0.75 kW) motor; this 10-head uses 1.5 HP (1.1 kW) and the 12-head 2 HP (1.5 kW). Between the smallest and largest machine in the range, rated capacity rises around five and a half times while motor size only doubles — which is why kWh per 100 kg of raw nut stays low even as you scale up.

This approach keeps maintenance simple. A processor running a mix of head counts on their factory floor is working with the same blade steel and largely the same wear parts across every machine, which simplifies spare parts stocking and operator training. Motors are the one component to specify per machine rather than treat as common stock.

How cutting happens

Nuts arrive at the machine already steamed, which softens the shell and improves separation from the kernel. An operator loads one nut into each cup by hand. As the shaft turns, each cup carries its nut through the blade at a fixed height and angle, scoring the shell along its natural seam rather than crushing it. This consistency — every cup passing the same blade at the same position — is central to why outturn stays predictable across a full shift rather than drifting as fatigue sets in.

Once a cup clears the blade, the operator opens the shell and removes the kernel, then reloads the cup for its next pass. With ten cups in continuous rotation, the machine keeps the blade working steadily rather than sitting idle between individual nuts, which is the main reason a 10-head model outproduces a lower head-count machine running the same motor speed.

Sizing this machine for your line

A 10-head machine suits mid-size processing operations that need meaningful daily volume but want to stay in manual or semi-manual cutting rather than moving to automatic equipment. Getting close to the top of the 200–240 kg/hr range generally means running two operators — one focused on loading cups, one on unloading and kernel extraction — so the cutting cycle itself never has to wait on manual handling.

Because outturn depends heavily on RCN quality and steaming consistency ahead of the cutting stage, processors evaluating a 10-head machine should also look at their upstream steaming and sizing process. A well-conditioned nut feeding a well-maintained blade is what gets a factory close to the 76% figure we quote for this model; inconsistent steaming or a worn blade will pull actual results below it.

Built for Vietnam-to-export operations

OUTTURN manufactures this machine factory-direct out of Bình Phước, Vietnam, in the heart of the country’s cashew-growing region. Processors across Africa, Asia, and South America run OUTTURN machines as part of export-oriented operations, and the 10-head model is a common step up for facilities scaling from a handful of manual cutters toward a larger, still hands-on cutting floor.

Frequently Asked Questions — 10-Head Cutter

What size motor does the 10-head machine use?
The 10-head runs a 1.1 kW (1.5 HP) motor. Our 2-, 4-, 6- and 8-head machines all use a 1 HP (0.75 kW) motor, and the 12-head steps up again to 2 HP (1.5 kW). OUTTURN's cutting machines scale mainly by adding cutting stations rather than by fitting proportionally bigger motors, because each cup only needs a brief, low-force pass through the blade — so power steps up modestly at the larger head counts while throughput rises much faster. That keeps electricity cost per 100 kg of raw nut low across the range.
How many operators does a 10-head machine need to hit 200–240 kg/hr?
Throughput on any head-count model depends on how quickly operators load and unload cups, not just the machine's mechanical speed. A 10-head machine is typically run by one to two experienced operators working the full row of cups; factories aiming for the top of the 200–240 kg/hr range often assign a second person to unloading and kernel extraction so cup loading never stalls the cutting cycle.
What outturn percentage should I expect from this machine?
We rate the 10-head machine at approximately 76% outturn under normal operating conditions, meaning roughly that share of kernel weight is recovered whole or in usable pieces relative to the cut RCN. Actual outturn varies with nut variety, steaming quality, moisture content, and operator skill, so treat 76% as a realistic working estimate rather than a guarantee.
Do the raw cashew nuts need to be steamed before using this machine?
Yes. Steaming or boiling the RCN beforehand softens the shell so it separates more cleanly from the kernel during cutting, which reduces kernel breakage and improves outturn. Feeding unsteamed, hard-shelled nuts into the machine will increase blade wear and produce a higher share of broken kernels.
How does the 10-head model compare to OUTTURN's 6-head or 8-head machines?
The 10-head machine sits toward the upper end of OUTTURN's 2-to-12-head lineup and is built for processors who need more throughput than a 6- or 8-head machine can deliver but are not yet ready for a fully automatic line. The cutting mechanism, blade material, and wear parts are the same across the range — the main differences are more cups per cycle, which raises the kg/hr ceiling and requires a correspondingly larger operator team, and a slightly larger motor: 1.5 HP here against the 1 HP fitted to the 6- and 8-head models.
Can the blades be replaced or sharpened in the field?
The cutting blades are special alloy steel and are designed to be field-replaceable. Over time and heavy use, blades will dull and should be swapped rather than run past their useful edge, since a worn blade tends to tear shells instead of cleanly scoring them, which lowers outturn. We recommend keeping spare blades on hand for a 10-head machine given its higher cycle count per hour.

Get a Complete Line Specification

Tell us your daily RCN volume, origin, and shift hours — we'll recommend the right configuration, factory-direct from Vietnam.