Skip to content
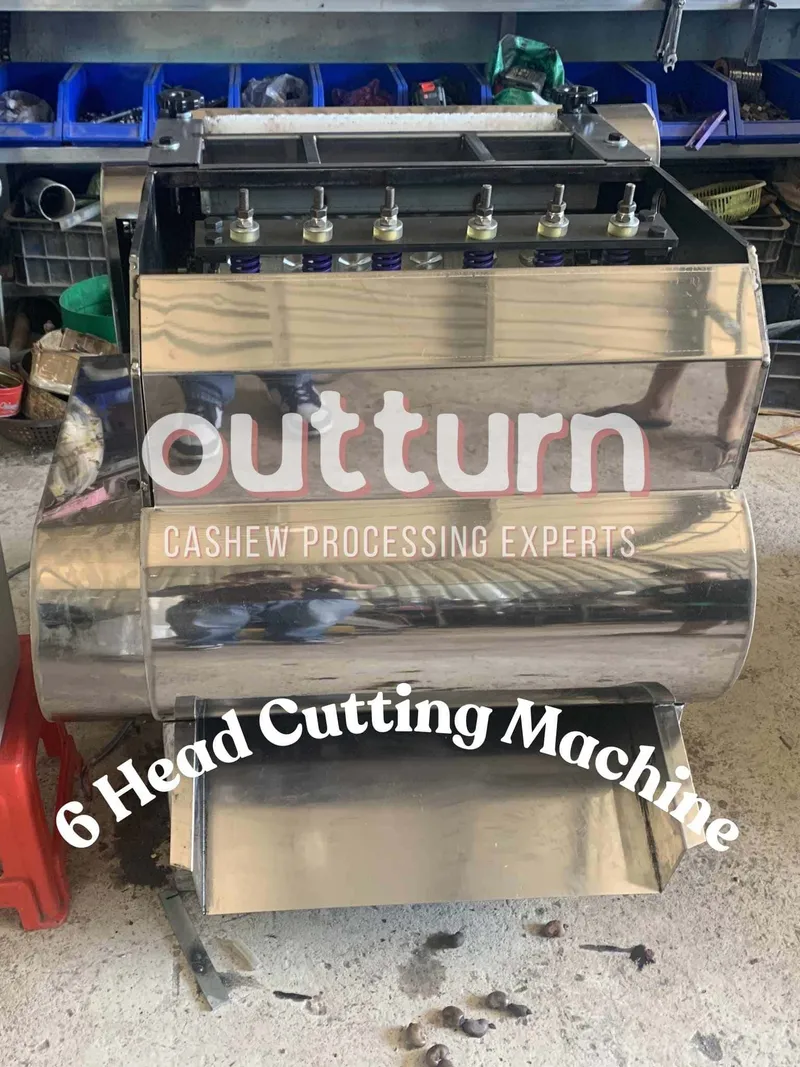
OUTTURN 6-head cashew nut cutting machine with six rotary cutting stations on a factory floor
120–150 kg/hrUp to 74% Outturn

6-Head Cashew Nut Cutting Machine

SKU: OUTTURN-CCM-6H

Factory-Direct Pricing — Request a Quote

Motor Power
0.75 kW (1 HP), single-phase induction motor
Cutting Heads
6 rotary cutting stations
Rated Capacity
120–150 kg/hr raw cashew nuts (dry basis)
Average Outturn
Approx. 74% whole kernel (operator-dependent)
Blade Material
Special alloy steel, replaceable
Power Supply
220V single-phase, 50Hz
Machine Weight
Approx. 145 kg
Footprint (L x W x H)
Approx. 1.4 x 0.7 x 0.95 m
Broken Kernels (Cutting Stage)
Under 3%; under 1% with well-graded, evenly steamed RCN
Uncut Nuts (Cutting Stage)
Under 5%; lower still by reducing motor speed
Blade Care
Clean daily, sharpen weekly, replace every 2–3 months depending on workload
Spare Parts
Made in-house at our factory: genuine parts at factory-direct prices

How the 6-Head OUTTURN Cutting Machine Works

A step-by-step look at how raw cashew nuts move through the 6-head machine's rotary cutting cycle, from loading to kernel extraction.

  1. 1

    Load the raw cashew nut

    The operator places a pre-treated (steamed or roasted) raw cashew nut into an empty cup on the rotating head assembly.

  2. 2

    Cup indexes toward the blade

    As the operator loads the next cup, the previously loaded cup rotates into position under the fixed cutting blade.

  3. 3

    Blade separates shell from kernel

    As the cup rotates past the fixed, angled blade, the blade scores the shell along its natural seam and opens it, exposing the kernel inside.

  4. 4

    Cup rotates away for unloading

    The head assembly continues turning, carrying the cut nut away from the blade and presenting it to the operator for extraction.

  5. 5

    Operator extracts kernel and shell

    The whole kernel is lifted free of the two shell halves and placed in a collection tray, with shell waste dropped separately.

  6. 6

    Cycle repeats across all six heads

    Because the rotation is continuous rather than stop-start, up to six operators can work the machine in parallel, one per station, each keeping their own loading rhythm.

  7. 7

    Kernels move to the next processing stage

    Cut kernels proceed to peeling, drying, and grading, while separated shells are set aside for CNSL extraction or use as boiler fuel.

A mid-range workhorse for growing processing lines

Cashew processors who have outgrown a small manual line, but aren’t ready for a full automated cutting hall, tend to land on a 6-head machine. It sits at the midpoint of OUTTURN’s cutting range, sized for a crew of up to six operators working side by side, or fewer operators spread across the stations during quieter shifts. Rated at 120–150 kg/hr of raw cashew nut, it gives a processor a meaningful jump in daily throughput without the floor space, crew size, or capital outlay that an 8-head or larger installation calls for.

How the cutting cycle works

Every OUTTURN cutting machine, regardless of head count, uses the same rotary mechanism. Each of the six heads carries a cup sized to hold a single pre-treated raw cashew nut. As the head assembly turns, each cup passes in sequence through the blade plane, where a fixed, angled blade splits the shell along its natural seam as the cup rotates through it. The cup then continues rotating away from the blade, presenting the cut nut to the operator for kernel extraction, while the next loaded cup is already approaching the cutting position behind it. Because the six stations index continuously instead of stopping and starting, an operator working a station can settle into a steady load-cut-extract rhythm, with the mechanical rotation setting the pace rather than the operator racing a stationary blade.

Extracted kernels move on to peeling, drying, and grading; shell halves are collected separately, since cashew nut shell liquid (CNSL) and shell material carry their own resale or fuel value in many processing operations.

Sizing 120–150 kg/hr against a real production plan

Six heads translate to noticeably higher throughput than OUTTURN’s 2- and 4-head machines, without the plant footprint and staffing structure that come with 8 heads or more. When sizing a line, it helps to think in terms of raw nut input per shift rather than the headline capacity figure alone: sustained at 120–150 kg/hr across a typical operating day, a fully staffed 6-head machine processes several hundred kilograms of raw cashew nut, scaling down cleanly if fewer stations are staffed on a given day.

More cutting stations, modest steps in motor size

OUTTURN’s cutting machines span 2 to 12 heads. This 6-head unit runs a 1 HP (0.75 kW) motor, the same one fitted to the 2-, 4- and 8-head machines; only the two largest models step up, to 1.5 HP (1.1 kW) on the 10-head and 2 HP (1.5 kW) on the 12-head. What mainly changes across the lineup is the number of cutting stations rather than the power behind them — the motor’s job is to drive the rotating head assembly, not to add cutting force per station.

That keeps electrical demand modest across the whole range, so a processor stepping up from a 4-head machine to this 6-head model, or later to an 8-head, isn’t rewiring their shed for a heavier power draw — those four models all share the same 1 HP supply requirement, and motors are interchangeable between them. Moving up to a 10- or 12-head machine does mean a larger motor, so it is worth confirming your supply can carry it at that point.

Outturn is a system result, not just a machine spec

The 74% average outturn figure for this model reflects normal operating conditions: properly steamed or roasted RCN, blades kept in good condition, and operators who’ve had time to build cutting rhythm. Outturn on any cutting machine is shaped by more than the equipment itself — moisture content, nut variety, roasting or steaming consistency, and operator technique all move the number up or down. Processors comparing this figure against other equipment should read it as a realistic operating average rather than a fixed guarantee on every batch.

Frequently Asked Questions — 6-Head Cutter

How many operators does the 6-head machine need to run?
The machine is designed for up to one operator per cutting head, so a full crew is six people working simultaneously. Many processors run it with fewer staff during slower shifts by simply leaving some stations unattended, since each head cuts independently. Output scales roughly with how many stations are actively staffed, which gives a plant some flexibility as order volumes change.
What preparation do raw cashew nuts need before going into this machine?
Like all OUTTURN cutting machines, the 6-head unit is built for pre-treated raw cashew nut, typically steamed or drum/oil roasted and cooled to a workable temperature and moisture level. Feeding untreated nuts into the machine increases kernel breakage and accelerates blade wear. Consistent pre-treatment upstream is one of the biggest factors in whether a processor actually reaches the machine's rated outturn.
How does the 6-head model compare to OUTTURN's 4-head and 8-head machines?
All OUTTURN cutting machines, from 2 heads up to 12, share the same rotary cutting mechanism, and the 2-, 4-, 6- and 8-head models share the same 1 HP (0.75 kW) motor — capacity scales mainly with the number of cutting stations rather than motor power, with only the 10-head (1.5 HP) and 12-head (2 HP) needing a larger one. The 6-head sits in the middle of that range at 120–150 kg/hr, a step up from a 4-head line for processors who've outgrown it but don't yet need the floor space or crew size an 8-head or larger machine calls for.
What outturn rate should I actually expect from this machine?
Under normal conditions, with properly steamed or roasted RCN and reasonably experienced operators, the 6-head machine averages around 74% whole-kernel outturn. That figure moves up or down with nut variety, moisture content, pre-treatment consistency, and operator skill, since outturn is a result of the whole process, not the cutting machine alone. Treat 74% as a realistic operating average rather than a guarantee on every batch.
Can the cutting blades be replaced without sending the machine back to Vietnam?
Yes. Each of the six heads uses a special alloy steel blade that your team can swap on site. Clean the blades daily, sharpen them weekly, and replace them every 2–3 months depending on workload. OUTTURN makes replacement blades in-house, sized for each cutting head, and in-stock parts are dispatched within 48 hours of order confirmation.
What electrical supply does the 6-head machine require?
It runs on a standard 220V single-phase, 50Hz supply through its 0.75 kW motor. That's a modest, common connection for most processing sheds, rather than a three-phase industrial feed, which is one reason this head-count range is practical for small and mid-size operations without specialized electrical infrastructure.

Get a Complete Line Specification

Tell us your daily RCN volume, origin, and shift hours — we'll recommend the right configuration, factory-direct from Vietnam.